Explore our premium selection of high-purity plant protein isolates, concentrates, and functional botanical extracts engineered for global food, beverage, and supplement industries.
Comext Sunflower Seed Powder Food Ingredients Vegan Sunflower Seed Extract Sunflower Protein Powder
View Details
High Quality Food Grade Hydrolyzed Wheat Protein Powder Natural Extract Wheat Protein Powder Pure Wheat Protein 80%
View Details
Wholesale Hydrolyzed Pea Protein Powder Food Grade Nutrition Enhancer Widely Used in Health Supplements and Drinks
View Details
Chickpea Protein Food Grade High Performance Plant Protein for Modern Formulations
View Details
High Quality Low Price 90% Isolate Soy Protein Premium Grade for Meat and Dairy Alternatives
View Details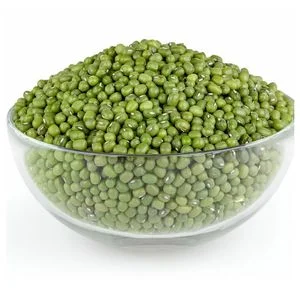
Bulk Organic Dried Green Gram Seeds High Protein Mung Beans Double Tongues Brand 12 Months Shelf Life Wholesale Vigna Beans
View Details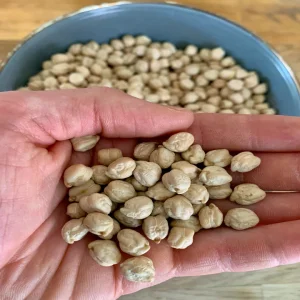
Dried Chickpeas/Garbanzo Beans, Source of Vegetarian Protein Premium Agricultural Sourcing
View Details
ISO Factory Supply Natrual Faba Bean Protein Isolate Powder 90%protein Natrual Vicia Faba Extract Vicia Faba Powder
View DetailsHangzhou Entry Bio Co., Ltd. stands at the forefront of the global plant-based protein revolution, driving rigorous scientific research and scalable industrial manufacturing.
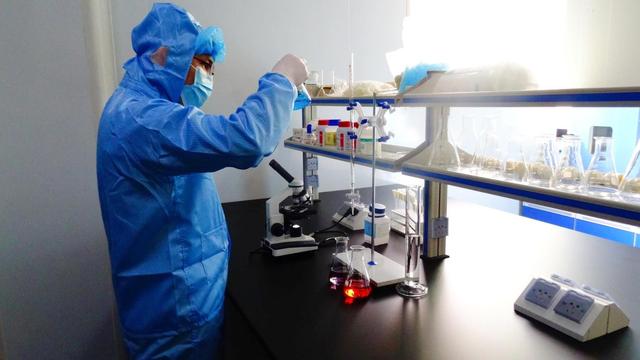
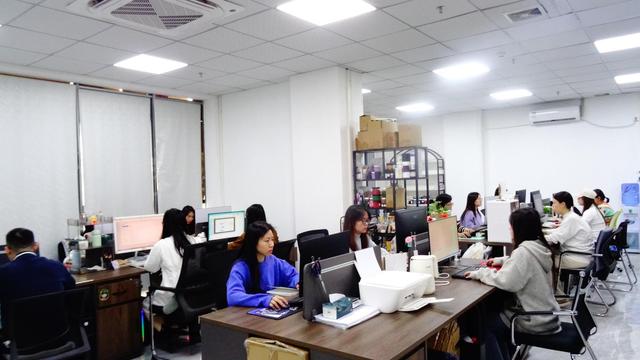
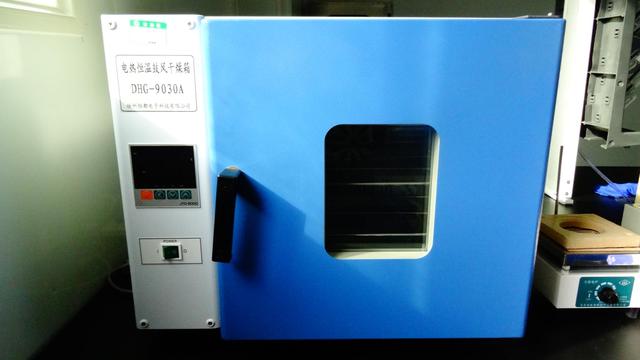
Hangzhou Entry Bio Co., Ltd. is a leading China vegetal protein manufacturer specializing in the research, production, and global supply of high-quality plant protein ingredients and food-grade protein solutions. With a strong commitment to innovation, quality, and sustainability, the company serves customers across the food, beverage, nutrition, and health industries worldwide.
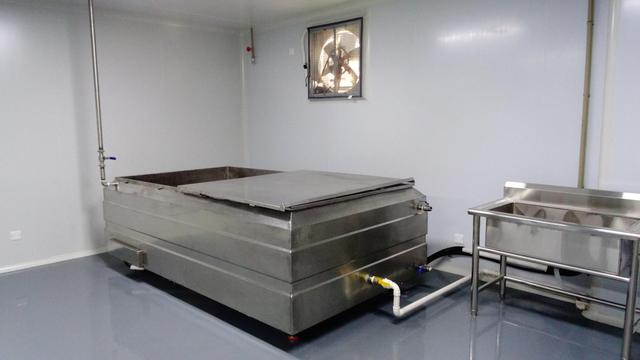
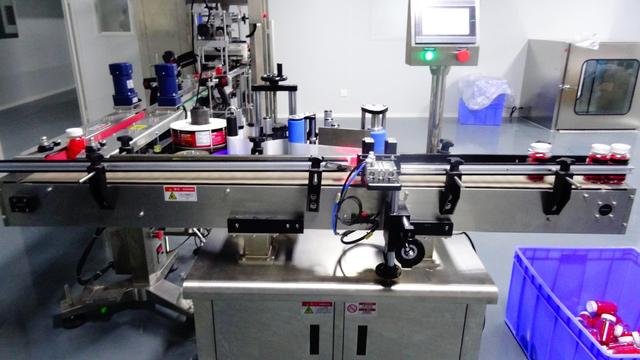
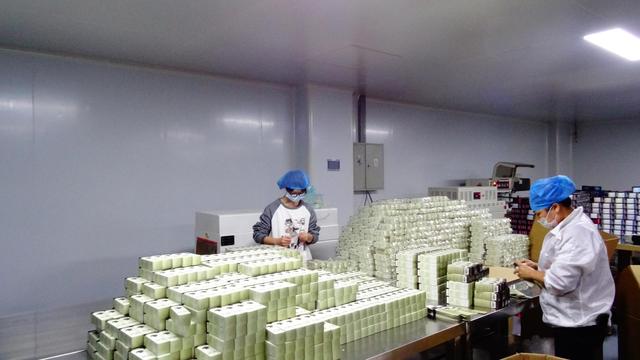
Leveraging advanced manufacturing technologies and strict quality management systems, Hangzhou Entry Bio Co., Ltd. offers a comprehensive portfolio of plant-based ingredients, including soy protein, pea protein, rice protein, textured vegetable protein, and customized protein blends. These products are widely used in meat alternatives, dairy alternatives, sports nutrition, functional foods, bakery products, beverages, and nutritional supplements.
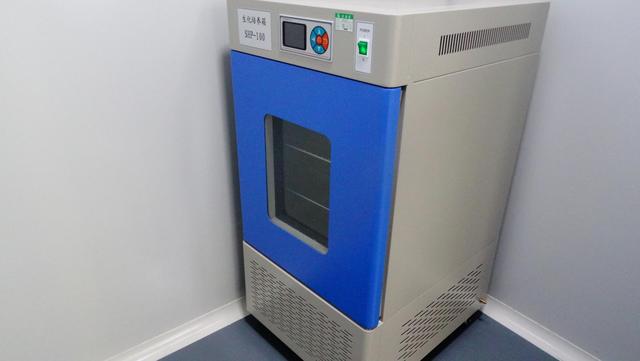
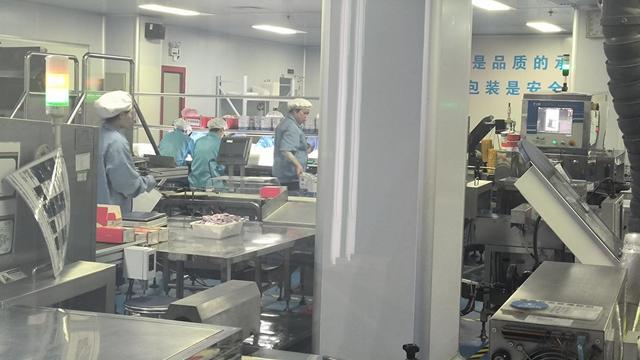
Quality and food safety are at the core of the company's operations. From raw material sourcing to finished product delivery, every production stage is carefully monitored to ensure consistent quality, purity, and performance. The company adheres to international quality standards and continuously invests in product innovation to meet the evolving demands of the global plant-based market.
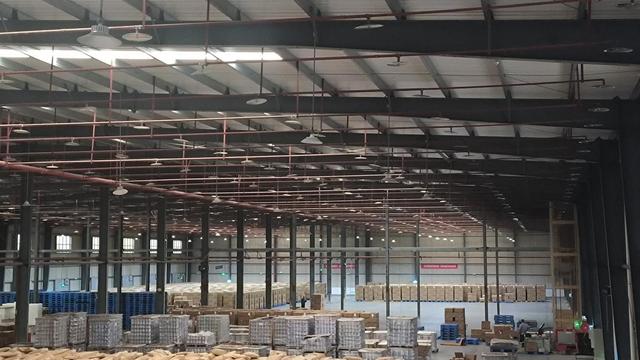
As a reliable plant protein ingredients supplier, Hangzhou Entry Bio Co., Ltd. also provides professional technical support and customized formulation services, helping customers develop competitive and market-oriented products. Backed by an experienced R&D team and efficient supply chain management, the company is capable of delivering tailored solutions for diverse application requirements.
Dedicated to promoting sustainable nutrition and healthy lifestyles, Hangzhou Entry Bio Co., Ltd. strives to be a trusted global partner for food manufacturers seeking premium vegetal proteins and innovative food-grade protein solutions.
Discover our advanced specialty proteins, microbial fermentations, and industrial-grade processing machinery built for high-throughput efficiency.
Oat Protein Isolate 80% Purity Plant Based Vegan Protein Powder Clean Label Formulation
View Details
Natural Food-Grade Chickpea Protein Isolate Powder Herbal Extract in Drum Packaging
View Details
Canola Oil Processing Equipment Oil Extraction and Refinery Workshop Industrial Solution
View Details
Mung Bean Protein Isolate Powder 70% 80% 85% 95% High Purity Botanical Source
View Details
Comext Spirulina 10: 1 Polysaccharides (PSP) 10-70% Beta-Carotene Food Additive Skin Conditioning Agent
View Details
AMULYN High Quality 100% Natural Mung Bean Protein Peptide Hydrolyzed Green Beans Peptide Powder
View Details
200tpd Multiple Crude Edible Oil Refinery Equipment Oil Refinery Technology with Auto Control System
View Details
Angeo Pro Yeast Protein Fermented High Yeast Protein Extract Powder Hydrolyzed Yeast Protein Powder
View DetailsA comprehensive analysis of market dynamics, manufacturing resilience, technological advancement, and compliance frameworks shaping the future of protein-rich grains.
The global demand for plant-based proteins has transitioned from a niche dietary trend to a core pillar of international food security and industrial formulation. Driven by shifting consumer preferences toward clean-label, allergen-free, and environmentally sustainable nutrients, protein-rich grains such as peas, chickpeas, faba beans, mung beans, and pseudocereals are experiencing unprecedented industrial adoption.
China remains the undisputed powerhouse of raw agricultural extraction and advanced refining. Hangzhou Entry Bio Co., Ltd. leverages integrated supply chain networks, automated processing workshops, and localized farming partnerships to ensure uninterrupted supply stability, cost competitiveness, and stringent traceability from farm to finished powder.
Looking ahead, enzymatic hydrolysis, green extraction technologies, and molecular modification will define the next generation of protein ingredients. Our R&D roadmap focuses on improving functional attributes such as solubility, gelation, and neutral taste profiles, unlocking new horizons for beverages, infant formulas, and clinical nutrition.
Protein-rich grain isolates are highly versatile. In North America and Europe, they dominate plant-based dairy analogues (milk, yogurt, cheese) and meat substitutes. In Asian markets, functional beverages, meal replacement shakes, and sports nutrition powders leverage mung bean and chickpea peptides for rapid absorption and clean nutritional profiles.
Navigating international food laws requires rigorous documentation. We provide full compliance packages including ISO, HACCP, Halal, Kosher, and Non-GMO certifications. Our technical support team assists clients with custom formulation, regulatory filing, and localized shelf-life testing to accelerate global market entry.
Expert answers to common technical, regulatory, and commercial inquiries regarding our plant protein manufacturing operations.
Our standard MOQ varies by product type, typically starting at 500kg for standard plant protein isolates and negotiable for custom hydrolyzed peptide blends to accommodate pilot runs and commercial launches.
We maintain dedicated processing lines and rigorous testing protocols to prevent cross-contamination. Most of our botanical proteins (pea, chickpea, mung bean) are naturally allergen-free, gluten-free, and Non-GMO.
Yes. Utilizing advanced enzymatic hydrolysis and physical restructuring, we tailor solubility, emulsification capacity, and viscosity to match specific food and beverage application requirements.
Our production facilities operate under ISO9001, HACCP, and GMP standards. Products are certified Kosher, Halal, and undergo third-party heavy metal and microbiological testing prior to shipment.
 Entry Biology