Explore our high-grade, sustainable, and customizable natural protein extracts engineered for global food and nutrition innovators.
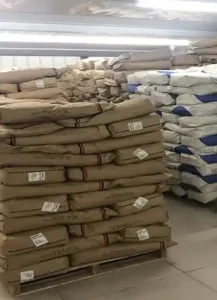
Plant-Based Protein Without Pesticide Residues and Gluten, ideal for clean-label applications.
Factory Natural Food Grade High-Purity Pea Protein Peptides for superior solubility and absorption.
Pure Natural Cosmetic Raw Material Cas 70084-87-6 with Free Samples and OEM Customization.

High Quality Supplements Seed Protein Pumpkin Powder 50% 60% offering the best wholesale price.
Factory Direct Supply for Food and Beverage industries, delivering exceptional nutritional profiles.
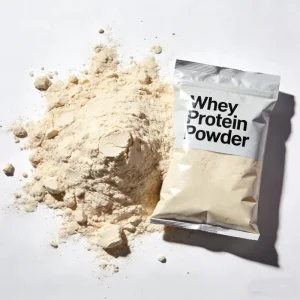
High-Quality WPI 90% 80% Whey Protein Isolate for Sports Gym and Health Nutrition, US/EU Compliant.
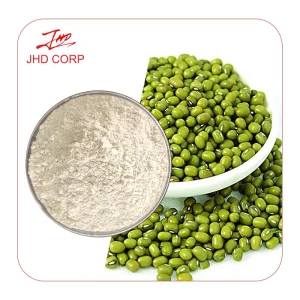
JHD Bulk 80% Isolate Mung Bean Protein Powder designed for functional foods and beverages.
Cost-effective, premium soy protein isolate optimized for large-scale industrial food processing.
Engineered for perfection, backed by decades of biochemical R&D and cutting-edge manufacturing infrastructure.
Hangzhou Entry Bio Co., Ltd. is a leading China vegetal protein manufacturer specializing in the research, production, and global supply of high-quality plant protein ingredients and food-grade protein solutions. With a strong commitment to innovation, quality, and sustainability, the company serves customers across the food, beverage, nutrition, and health industries worldwide.
Leveraging advanced manufacturing technologies and strict quality management systems, Hangzhou Entry Bio Co., Ltd. offers a comprehensive portfolio of plant-based ingredients, including soy protein, pea protein, rice protein, textured vegetable protein, and customized protein blends. These products are widely used in meat alternatives, dairy alternatives, sports nutrition, functional foods, bakery products, beverages, and nutritional supplements.
Quality and food safety are at the core of the company's operations. From raw material sourcing to finished product delivery, every production stage is carefully monitored to ensure consistent quality, purity, and performance. The company adheres to international quality standards and continuously invests in product innovation to meet the evolving demands of the global plant-based market.
As a reliable plant protein ingredients supplier, Hangzhou Entry Bio Co., Ltd. also provides professional technical support and customized formulation services, helping customers develop competitive and market-oriented products. Backed by an experienced R&D team and efficient supply chain management, the company is capable of delivering tailored solutions for diverse application requirements.
Dedicated to promoting sustainable nutrition and healthy lifestyles, Hangzhou Entry Bio Co., Ltd. strives to be a trusted global partner for food manufacturers seeking premium vegetal proteins and innovative food-grade protein solutions.
Discover our specialized hemp, sunflower, dairy protein options, and industrial processing machinery.
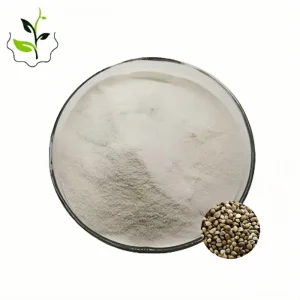
Best Price High Quality Hemp Seed Protein Powder packaged securely in 25kg bulk industrial sacks.
High-grade Whey Protein Isolate WPI 90% and Concentrate WPC 80% powder for maximum muscle recovery.
Specialized Whey Protein Isolate optimized specifically for advanced dairy applications and beverages.
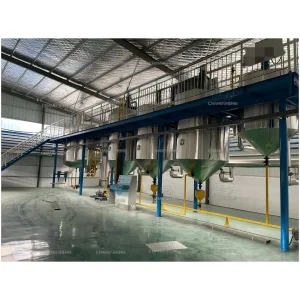
2-10td Crude Soybean Canola Groundnut Cooking Vegetable Oil Refining Equipment Machine Plant.
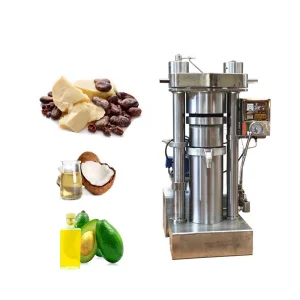
Cocoa Butter, Coconut, Canola Oil Presser, Flaxseed and Walnut Oil Extraction Processing Machine.
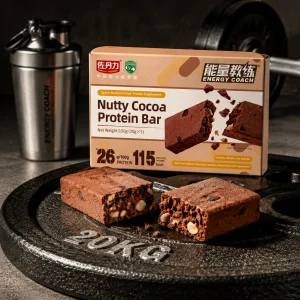
Protein Bar Factory Wholesale Dietary Nutrition Vegan Healthy Food for Health Management.
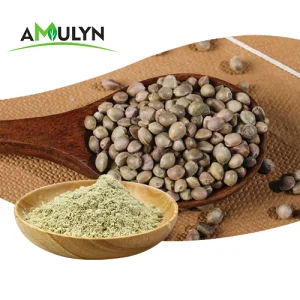
Non-GMO Natural Organic Hemp Seed Protein Powders specifically formulated for nutritional supplements.
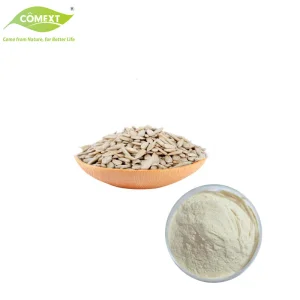
Comext Sunflower Seed Powder Food Ingredients Vegan Sunflower Seed Extract Protein Powder.
Pioneering the next generation of alternative proteins through molecular engineering and sustainable bioprocessing.
Our advanced R&D focus centers on proprietary enzymatic cleavage techniques. By breaking down complex plant macro-proteins into low-molecular-weight bioactive peptides, we dramatically enhance human digestive absorption rates (PDCAAS optimization) while eliminating bitter off-notes common in generic plant proteins.
Transitioning beyond traditional chemical solvent extraction, our facilities deploy closed-loop water recycling and subcritical fluid extraction technologies. This drastically reduces our carbon footprint, retaining full spectrum amino acid profiles without exposing raw inputs to harsh residues.
Tailored regulatory compliance and localized supply chain integration for North American, European, and Asia-Pacific markets.
All production lines operate strictly under HACCP, ISO22000, FDA registration, and EU food safety guidelines, ensuring effortless customs clearance and market entry for global brand owners.
Equipped with fully automated IoT monitoring, our smart factory ensures uncompromised lot-to-lot consistency, real-time tracking, and massive scale production capacity to buffer supply shocks.
From custom amino acid spiking and flavor masking to bespoke retail packaging, our technical team collaborates closely with your R&D department to accelerate time-to-market.
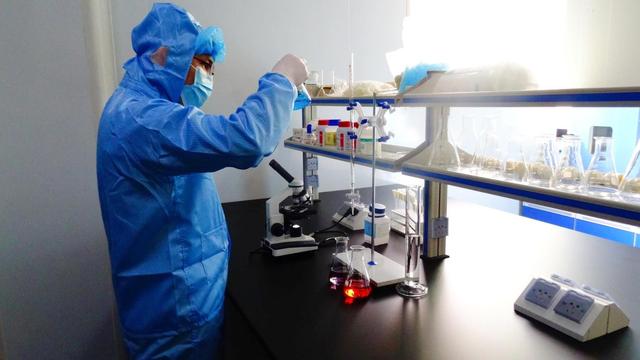
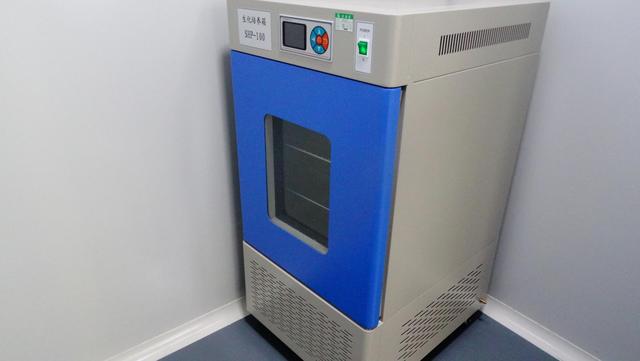
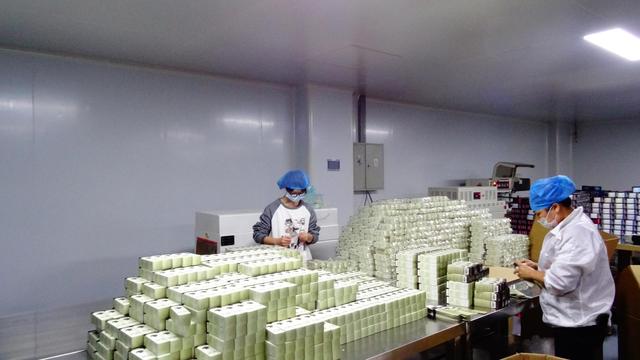
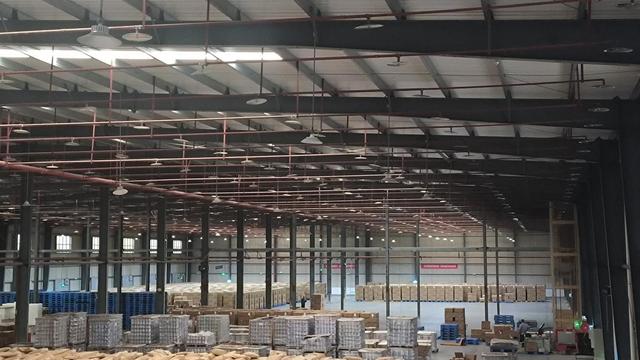
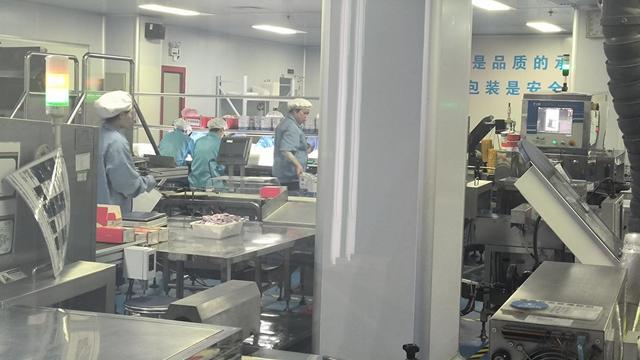
A visual tour of our state-of-the-art laboratory testing, cleanrooms, and automated extraction facilities.
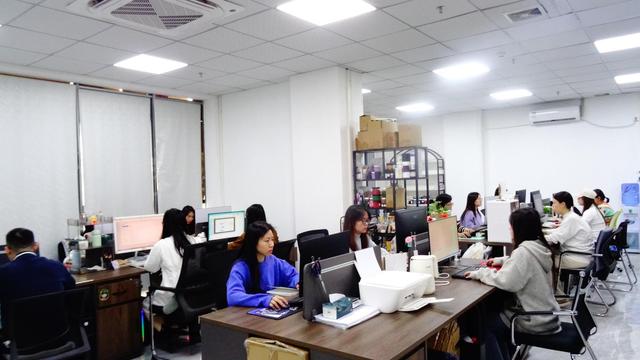
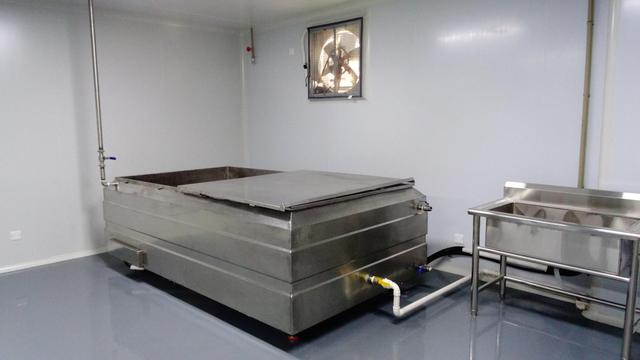
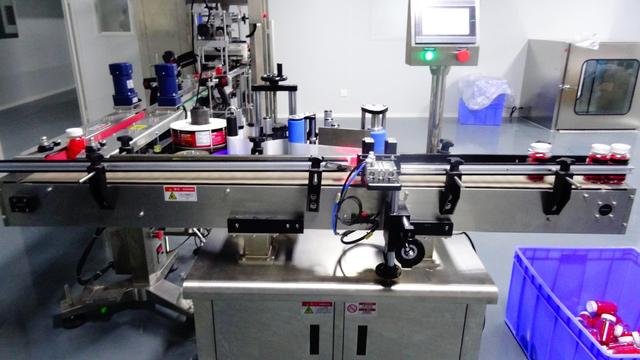
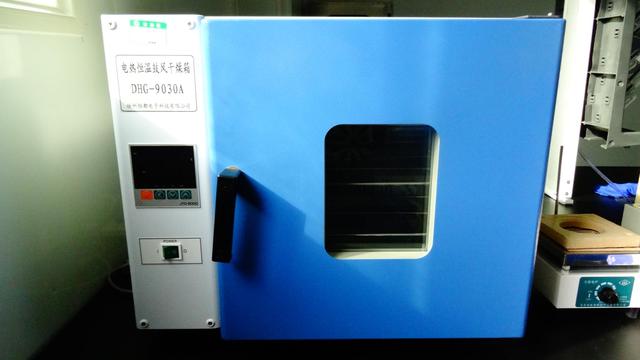
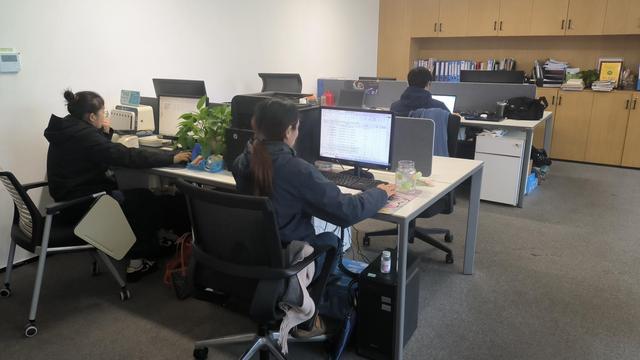
Expert answers regarding our natural protein manufacturing, custom formulation, and international shipping capabilities.
Our production facilities are fully certified by ISO22000, HACCP, GMP, and select organic certifications (NOP/EU). We provide comprehensive Certificates of Analysis (COA), allergen statements, and non-GMO project verifications with every batch shipped globally.
Yes. We specialize in OEM/ODM tailor-made formulations. Whether you need a specific ratio of pea and rice protein isolate, customized amino acid spiking, or targeted texture modification for plant-based dairy, our R&D team can develop and pilot-test prototypes for your brand.
Our standard MOQ typically starts at 500kg per product variant for bulk industrial delivery (e.g., 25kg bags). However, we fully support trial batches and sample testing for emerging brand partners—contact our technical sales team to discuss your project scale.
Through our integrated Factory 4.0 infrastructure, we maintain long-term direct contracts with premier non-GMO agricultural cooperatives for raw material sourcing. Automated processing and rigorous multi-stage lab testing guarantee 99.8% lot consistency year-round.
 Entry Biology